
IRONING WITH SIMPLIFY 3D

UPDATE - What's The Point?
Ironing is now included with Simplify 3D Version 5 which may well render this post irrelevant. However, it may still be of use to those who didn't want to pay for the 'upgrade', which in my opinion was a cash-grabbing con.
More to the point, in my view, the 'upgrade' simply isn't worth the money.
S3D (even version 5) is no longer the class-leading slicer it used to be and certainly isn't worth paying any money for. There are far better alternatives out there.
I now exclusively use OrcaSlicer or BambuStudio for all of my printing needs and removed S3D quite some time ago.
Update from November 2025. Version 5 of S3D hasn't received any purposeful updates in 2 years, proving it's a dead duck that briefly raised it's head to feed on the unwary or misguided.
There are a number of ways to achieve ironing in S3D and I have tried most of them. This post concentrates solely what I have come up with.
I will stress that my processes and settings are tailored around Creality Ender 3's 5's and CR10's with Micro-Swiss all metal hot ends and BMG clone extruders still in bowden configuration - don't copy my retraction settings (especially if on direct drive).
Let's jump in
First of all you have to create 2 processes for your print. The first does the main bulk of the print and is based on your default settings with (possibly) 2 modifications. The second produces a single top layer.
In my examples, I am using a standard 20mm XYZ calibration cube.
My top layer process is using a 0.08mm layer height. This is important, because you need to adapt the layer height of your main process so that it produces exactly the correct number of layers so the remaining top layer process only prints 1 layer.
Model height = 20mm
Top Layer = 0.08mm
20mm - 0.08mm = 19.92mm - This is the total height the main process needs to print. For my example, the main process 'was' using a 0.2mm layer height but if you leave it at the defaults, the ironing process will actually print 2 layers which is less than ideal. It's better than not having the process but is not as good as limiting the top to a single layer.
So, how do we get around this? 19.92 / 0.2 = 99.6 layers (S3D only creates 'full' layers so will only print 99 - the top process producing an additional layer to make up for the shortfall). So, we need to do the following calculation:
19.92mm (the height we need to print) / 99 (the number of complete layers) = 0.2012 (this is our adjusted layer height for the main process).
There will be people shouting 'magic numbers' at this point (on most Creality printers, the magic number is 0.04 which equates to the height the z will raise for one complete step of the Z axis motor). If the shouty people are capable of tramming their bed so the first layer coincides with the start of a step (first flaw of the magic number principle), good on 'em. But, they are also ignoring micro-stepping (second flaw of the magic number principle) so 'magic numbers' are now really a pile of bollocks.
The only changes we need to make to the main process are to adjust the layer height and tell the process to stop printing at the point the top process takes over.
Let's look at those settings. I've included all of my settings in case they are of use but will indicate the areas you need to concentrate on. These are my settings for my printers. Consider them as a basis of an idea and not exact settings that are going to work in every situation - tweaking will be required!
Main Process
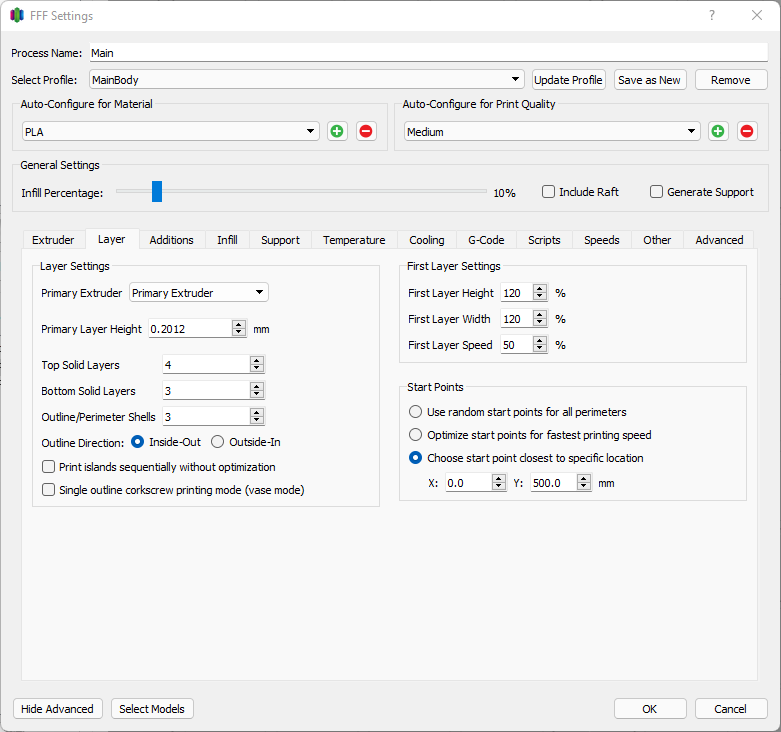
For the main process, you only need to modify 2 things. On the layer tab, change the Primary Layer Height to 0.2012 (calculated above):
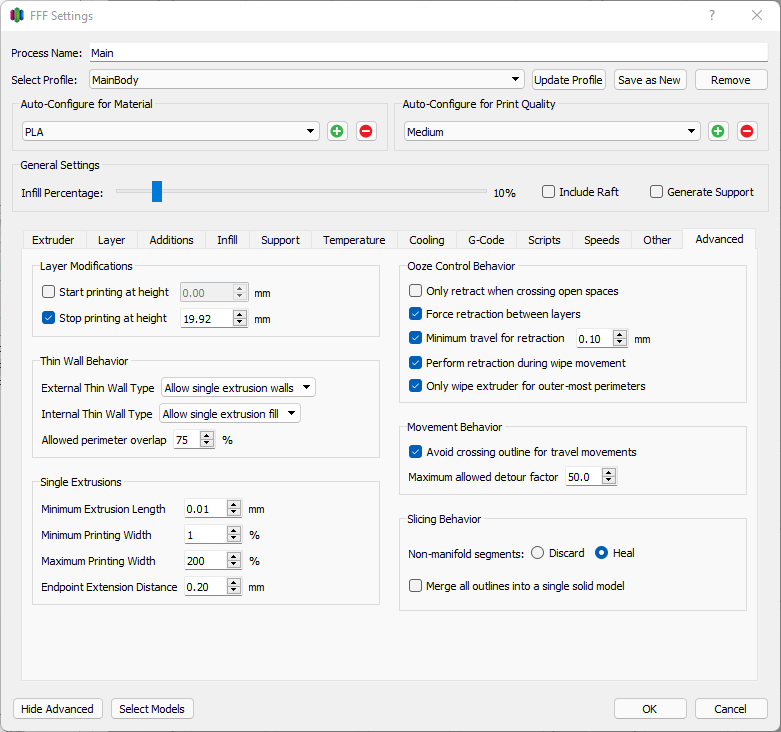
Then, on the Advanced tab, tell the slicer to stop printing the main process at 19.92mm in the Layer Modifications area:
Ironing Process
Top layer ironing is achieved by a number of settings:
Extruder Tab:
- Extrusion Multiplier: 1 - this works for my printers and filament. You may need to increase/reduce this number.
- Extrusion Width: 0.3mm (using a 0.4 nozzle). This produces a finer outer wall to the ironing process.

Layer Tab:
- Primary Layer height = 0.08mm
- Top Solid Layers: 0
- Bottom Solid Layers: 0
- Outline/Perimeter Shells: 1
- First Layer Settings: 100% for Height/Width/Speed

Infill Tab:
This is where most of the magic happens!
- Infill Pattern: Rectilinear
- Interior Fill Percentage: 100% (this is the ironing so needs to be solid)
- Outline Overlap: 75% (you want some decent overlap on the outer wall)
- Infill Extrusion Width: 40% (equates to a 0.12mm line width)
- Minimum Infill Length: 0.5mm (short bits needed!)

Speeds Tab:
- Default Printing Speed: 10mm/s
- Outline and solid infill underspeed: 100% (we've done enough math so 100% allows the default printing speed to control everything on the ironing layer)

Advanced Tab:
- Start printing at height: 19.92mm - In the example, the print is 20mm high, so we start one 0.08mm layer below the top.
- Internal Thin Wall Type: Allow single extrusion fill
- Allowed perimeter overlap: 50%
- Single Extrusions: I've meddled with so many settings, I no longer know if this has any effect but I'd suggest copying the settings below!

Slicing:
Once you have created both processes, you need to ensure that both are selected when you slice (the pop-up allows you to do this).
The images below show what you should see, compared to a standard, single process, slice.


Results
So, is all this fannying around worth it? In certain circumstances I believe they are but I will leave you to decide!
Left: Standard Process | Right: Using the procedure described above
Final THoughts
I put this post together in response to questions of the Simplify 3D Users Facebook group. The processes included are based upon settings I use every day for a very specific application and are tuned for a specific brand and colour of filament. I didn't perform temperature and flow calibration on the filament used in the test prints and, looking at the close ups of the prints, I really should have done so! There are some small gaps between the top layer extrusions on the non-ironed print. This may be down to either temperature or flow (extrusion multiplier). I may have also been printing the base process a bit fast!
In addition, the outline overlap of the ironing layer looks as if it can be reduced slightly. You can see some very fine jagged edges around the Z. I couldn't actually see any of these defects 'in the flesh' but that's what 50-odd year old eyes do for you!


Comments